-
Used Mazak CNC Mill: With Mazak Support or Without?
-
The Framework I Use Before Any Used Machine Purchase
-
Dimension 1: Acquisition Price vs. Total Cost
-
Dimension 2: Condition Risk and Prevention Over Cure
-
Dimension 3: Tooling and the 1 2 Indexable End Mill
-
Dimension 4: Are VMC Hooks Good? A Cost-First Answer
-
Dimension 5: Mazak Support Response Time and Downtime Cost
-
When to Choose Which
Used Mazak CNC Mill: With Mazak Support or Without?
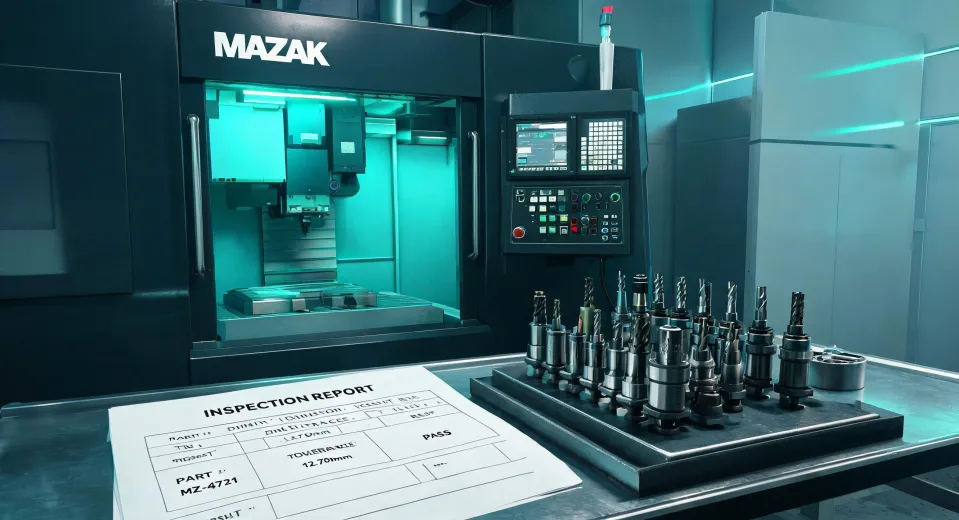
I'm a procurement manager at a 230-person precision machining company. I manage about $1.4 million every year for machines, tooling, and support contracts. Over the past seven years, I've logged every quote, every invoice, and every 'free' offer that ended up costing us. So when someone asks me about buying a used Mazak CNC mill, I don't lead with the sticker price. I lead with the total cost of ownership.
This is a comparison between two ways to get the same basic asset: a used Mazak CNC mill. Option A is the machine with an official Mazak support agreement. Option B is the same machine bought as-is, with no manufacturer-backed service plan. I'll compare them the way I'd compare any vendor option: acquisition price, condition risk, support response, tooling, and the small details that show up later. Prices mentioned are from quotes I have on file as of February 2025; verify current rates before you budget.
The Framework I Use Before Any Used Machine Purchase
In Q4 2024, I priced a used Mazak VCN-530C through a dealer that offered a Mazak support plan, and the same model from a private seller two states away. Dealer price: $86,000. Private price: $59,500. Looks like a $26,500 difference. Not so fast.
My total-cost spreadsheet adds shipping and rigging, a ballbar check, control parameter backup, tooling test cuts, and the cost of being down during the first month. By the time the private-machine freight, the independent inspection, and a replacement spindle drive were added, the 'cheap' machine was $93,170. The dealer-sourced machine with support? $91,400. The cheaper quote lost by $1,770.
That's the pattern I keep seeing. The support plan rarely turns a good machine into a bad deal. It keeps a bad surprise from becoming a budget disaster.
Dimension 1: Acquisition Price vs. Total Cost
Some shops buy a used Mazak CNC mill because they have a strong in-house maintenance team. If that's you, the private seller route might be logical. But I've also watched shops use that logic to skip a $2,500 inspection on a $60,000 machine. That is a 4% hedge on a machine that can burn $14,000 in tooling during one bad setup. Not ideal. Workable? No, it's a risk.
One quote that hurts:
I said we need full support. They heard we'll send a manual. Result: two weeks of ripple delays while I waited for a parameter file.
That was from a third-party reseller, not Mazak. Official Mazak support is different. You call, you get a case number, and they can pull the machine's service history from the serial number.
Dimension 2: Condition Risk and Prevention Over Cure
The best investment on any used VMC is not an extended warranty. It's a pre-purchase inspection. Per the machine tool accuracy standard ISO 230-2, you measure positioning deviation with a laser interferometer. That catches axis wear before it becomes a geometry problem. Most used Mazak mills are solid, but 'solid' doesn't mean 'no prior crash history.'
I have a scar from not following my own rule. Looking back, I should have paid for a full ballbar test on a used VMC. At the time, the auction price looked too good to turn down. The machine cut a test part that looked fine, but the circle was slightly lobed. A 0.0012 inch issue in the Y axis, nothing in X. That cost us $1,200 in scrapped parts and a full fixture re-fit. Five minutes of verification would have caught an axis compensation error. Five days of correction later, I got the point: prevention is cheaper than correction.
Dimension 3: Tooling and the 1 2 Indexable End Mill
Here's where a used Mazak CNC mill and a cheap tooling plan can quietly eat your savings. Let's talk about the 1 2 indexable end mill—the workhorse for milling steel on a VMC. The tool body is usually $95 to $140 in our last stock order. The real cost is in the inserts. And when we talk carbide insert coatings, that's where the decision gets interesting.
We order AlTiN-coated carbide inserts for most stainless and alloy steel work. For abrasive jobs, especially cast iron or high-silicon aluminum, a CVD-coated grade often lasts longer. Uncoated carbide has its place: roughing at low speeds, heavy scale, interrupted cuts. But at normal CNC speeds, coating pays for itself. In one test on a Mazak VCN, we ran the same 1 2 indexable end mill with uncoated carbide inserts on a 4140 job. The uncoated inserts lasted about 28 minutes before edge wear. The AlTiN-coated version lasted 47 minutes. Cost per insert: $2.10 vs $4.80. Cost per cubic inch of metal removed: the coated inserts were still 18% lower.
So my answer isn't 'always buy coated.' It's 'put coatings in the TCO sheet.' The machine you choose will have a spindle taper and speed range that dictates which 1 2 indexable end mill geometry you can run. That's a support question as much as a tooling one.
Dimension 4: Are VMC Hooks Good? A Cost-First Answer
Let's address the search query that sounds weird but keeps showing up: are VMC hooks good? I interpret 'VMC hooks' as the retention system in a vertical machining center that holds the tool holder in the spindle. That includes the drawbar fingers, the pull stud, and sometimes the hook-style clamp inside the spindle. The answer depends on condition, not on the name.
A pull stud that doesn't match the spindle taper angle can cause tool holder slippage. A worn drawbar hook can let the tool holder drop or pull lopsided. That's a $35 part causing a $14,000 spindle repair if it fails. So, are VMC hooks good? The OEM hooks are good when they're within spec. Aftermarket hooks can be fine, but verify the grade and the angle tolerance. We almost bought a box of cheap pull studs for our Mazak, and I say 'almost' because I caught the spec change at the last minute. Dodged a bullet. The aftermarket studs had the right thread pitch but the wrong head profile, and the drawbar wouldn't engage properly.
If you're searching 'are VMC hooks good' because you're looking at a brand named VMC, I can't speak for every product with that name. But here is the principle: the retention system is a wearing part, not a commodity. Measure it, buy from a source that gives you a tolerance and a material spec, and you'll avoid the kind of surprise that turns a good used-Mazak deal into a painful lesson.
Dimension 5: Mazak Support Response Time and Downtime Cost
We had a behavior in our shop called 'work around it.' That's normal for a 30-year-old machine, but not for a used machine you're still paying for. With a Mazak support plan, a call on Tuesday brought a technician on site Thursday. Diagnostic fee? Zero. The part was in their van. Without support, the same issue took three weeks: my maintenance manager found a local independent tech, I approved a $3,900 estimate, then we waited for parts. The machine made zero parts for 11 days. At our loaded shop rate of $150/hour, that's $13,200 of opportunity cost. The support contract cost $4,500 for the year.
The most frustrating part is that it's not the repair bill that hurts. It's the blank calendar. You'd think a used Mazak from the same generation would be predictable. It is—until the one thing that catches you. That's why I treat Mazak support as a line item in the operating budget, not a one-time add-on.
When to Choose Which
If your shop has a maintenance person who knows Mazak controls, and you've verified the service history on a used Mazak CNC mill, you might be fine without the official Mazak support agreement. That's the self-insured route. I respect it. I've seen a few shops do it successfully.
If you don't have that in-house knowledge, or if your customer lead times leave no room for a two-week surprise, buy the support plan. Or set aside a contingency fund equal to 15% of the machine price. That, in my experience, is the minimum buffer. So glad I made that rule after our 2023 incident. We almost skipped the support contract on a used Mazak VMC. Instead, we bought the one-year plan, and it paid for itself when a spindle thermistor failed in month six.
5 minutes of verification beats 5 days of correction.
Buying a used Mazak is not a gamble if you treat it like a vendor decision: compare total cost, check the details, and pay for prevention. The best machine purchase I've made wasn't the one with the lowest quote. It was the one where I knew exactly what could break—and who was going to answer the phone when it did.